Should you use argon or nitrogen for handheld laser welding?
For most workshops welding different metals, argon is the more versatile starting choice. Nitrogen can be a cost-effective alternative for certain stainless steel and carbon steel applications, provided the welding process is tested and approved.
The difference is not just gas price. Shielding gas can affect weld-pool behavior, porosity, surface appearance, and the chemical composition of the finished weld.
A shop producing stainless steel cabinets may have different gas requirements from one welding aluminum enclosures or corrosion-resistant components.
For buyers using a handheld laser welder, the best starting point is to match the gas to the material and required weld quality.
| Material | Argon | Nitrogen | Starting Recommendation |
|---|---|---|---|
| Stainless Steel | Widely applicable | Suitable for selected, qualified applications | Argon first; test nitrogen |
| Carbon Steel | Reliable starting option | Possible with an approved process | Compare on actual parts |
| Aluminum | Preferred for routine welding | Not a general-purpose substitute | Argon |
| Titanium | Appropriate inert shielding | Not suitable as a routine substitute | High-purity argon |
This comparison helps narrow the choice, but final gas selection should follow the material grade, laser-welding system, and any applicable welding procedure specification (WPS).https://www.youtube.com/embed/hfbQzcDIJOk
1. What Is the Difference Between Argon and Nitrogen?
Both gases are used to keep atmospheric oxygen and moisture away from the molten weld pool. However, they behave differently at welding temperatures.
Argon: Versatile and Chemically Inert
Argon is an inert gas. Under normal laser-welding conditions, it does not chemically react with the molten metal.
Its main advantage is versatility.
Argon is widely used with stainless steel, carbon steel, aluminum, and other alloys, making it a practical choice for fabrication shops working with several materials.
It can help protect the weld pool from oxidation and reduce contamination caused by surrounding air.
For a fiber laser welder, argon is particularly attractive when the operator frequently changes between different materials.
The main disadvantage is cost. In many markets, nitrogen can be supplied more economically, especially when high-volume gas delivery is available.
However, the actual difference depends on local cylinder pricing, rental fees, delivery, and gas consumption.
Nitrogen: Cost-Effective but Material-Dependent
Nitrogen can also provide effective atmospheric shielding, but it is not chemically inert at welding temperatures.
Depending on the alloy, nitrogen can dissolve into the weld pool and affect its microstructure.
This is not always harmful. Some stainless steel laser-welding studies have shown improved weld-pool behavior or reduced porosity under nitrogen shielding.
However, the same result should not be assumed for every stainless grade or welding setup. Research on duplex stainless steel also shows that nitrogen shielding can change the ferrite-austenite balance, making process qualification important.
For manufacturers performing repeatable welding on one approved material, nitrogen may offer a useful cost advantage.
For mixed-material workshops, argon is usually the simpler starting choice.
Does Shielding Gas Change Weld Quality?
Yes, but neither gas automatically produces a stronger or deeper weld.
Penetration, porosity, and bead appearance also depend on laser power, travel speed, focus, joint fit-up, and gas delivery.
A nitrogen-shielded stainless weld may perform well under one validated process, while another application may require argon to meet its quality requirements.
The best shielding gas is the one that delivers an acceptable weld on your actual material—not the one that performs best in an unrelated test.
2. Which Shielding Gas Should You Use for Each Metal?
Material selection is the most important factor when comparing argon and nitrogen.
A gas that works well on a stainless steel enclosure should not automatically be used on an aluminum component.
Stainless Steel: Argon or Qualified Nitrogen
Both argon and nitrogen can be considered for selected stainless steel laser-welding applications.
Argon is a practical starting choice for mixed fabrication, particularly when the shop already uses it for several metals.
Nitrogen may be worth testing for repeatable austenitic stainless steel work, including some 304 applications, when the machine manufacturer and welding requirements permit it.
The potential advantage is reduced shielding-gas cost without necessarily sacrificing acceptable weld quality.
However, stainless steel is not one single material category.
A decorative 304 stainless steel cabinet and a corrosion-critical duplex stainless steel component may require different welding procedures.
For corrosion-sensitive components, verify the required metallurgy, mechanical properties, and corrosion performance before substituting nitrogen for argon.
For general stainless fabrication, start with the approved gas and consider nitrogen only after confirming its performance on the actual grade and joint.
Carbon Steel: Compare Gas Cost and Weld Results
Carbon steel is another material where nitrogen may be considered in certain laser-welding applications.
For routine fabrication, argon provides a conservative starting point.
If your shop performs large volumes of repeatable carbon steel welding, comparing an approved nitrogen process can make financial sense.
However, cost should not be the only consideration.
Nitrogen uptake and weld properties can vary with steel composition and process conditions. A change of shielding gas may therefore require testing or requalification.
For a laser welding machine used on steel frames, brackets, and enclosures, compare completed weld quality and gas consumption rather than cylinder price alone.
Galvanized steel requires an additional consideration: zinc coatings in the weld zone can contribute to porosity and hazardous fumes. Changing from argon to nitrogen does not eliminate the need for appropriate surface preparation and fume extraction.
Aluminum: Choose Argon First
For ordinary handheld laser welding of aluminum, high-purity argon is the preferred starting gas.
Aluminum is already challenging because of its reflectivity, thermal conductivity, and oxide layer.
Nitrogen can react with molten aluminum under certain conditions and may form aluminum nitride, potentially changing the weld’s properties.
Although specialized industrial laser-welding research has investigated nitrogen shielding on aluminum, those results should not be treated as permission to substitute nitrogen on a normal handheld welding setup.
For aluminum fabrication, focus on clean material, suitable filler wire, correct focus, and stable argon shielding.
If porosity occurs, check the surface, gas delivery, and welding parameters before experimenting with another shielding gas.
3. How Much Shielding Gas Flow Do You Need?
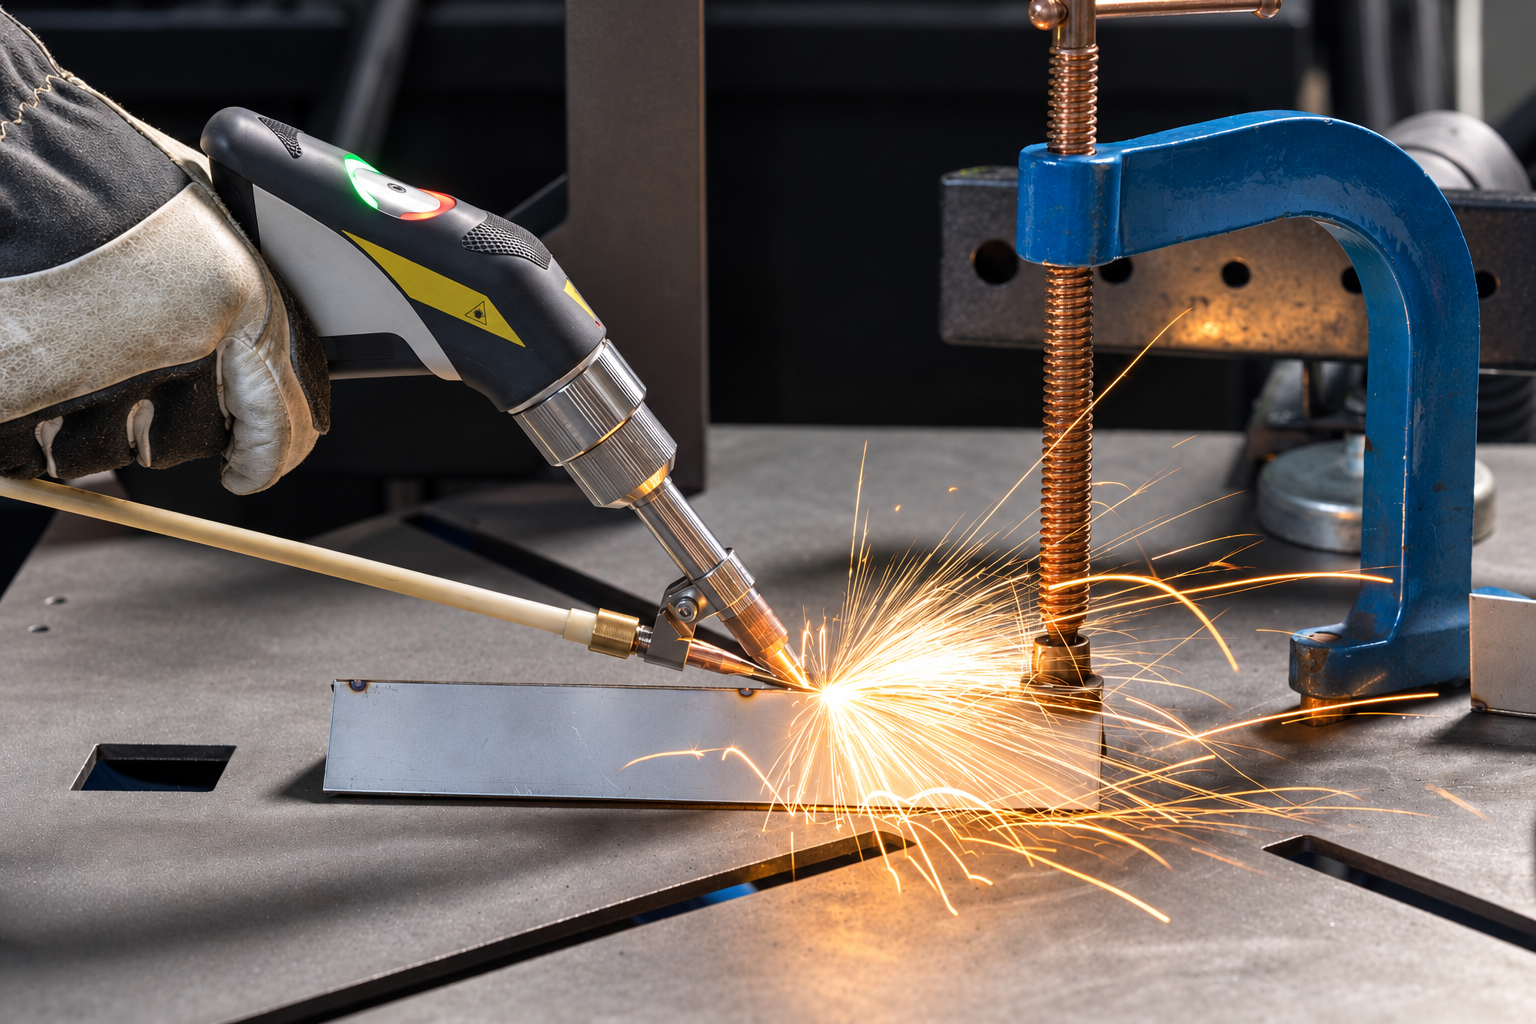
Selecting the right gas is only half the process for your laser welding equipment.
Poor gas delivery can cause oxidation and porosity even when the cylinder contains the correct shielding gas.
Start With the Manufacturer’s Flow Range
There is no single flow setting that works on every handheld laser welder.
The correct flow depends on nozzle size, nozzle position, welding speed, and surrounding airflow.
Some handheld laser-welding systems use approximately 15–25 L/min as an initial reference range, but this should not be treated as a universal requirement. Air Products, for example, publishes different illustrative flow values for argon and nitrogen in its handheld-welding guidance.
Use the flow range specified for your machine and welding head, then verify coverage during a sample weld.
Too little flow can allow atmospheric air into the weld zone.
Excessive flow may disturb the molten pool or become turbulent, reducing shielding effectiveness.
The objective is stable coverage, not maximum gas consumption.
Check Nozzle Position and Workshop Airflow
Shielding performance also depends on how the gas reaches the weld.
A nozzle positioned too far from the workpiece may allow the gas to disperse before adequately protecting the molten pool.
Spatter buildup, damaged nozzle openings, and inconsistent torch angles can also affect delivery.
Workshop fans, open doors, and poorly positioned extraction systems may disturb the shielding gas.
Before increasing flow, inspect the nozzle and reduce disruptive drafts while maintaining appropriate fume extraction.
Check Gas Purity and Weld Appearance
Gas purity should meet the requirements specified for your welding application.
High-purity gas, often 99.99% or higher where required, is a common choice for clean laser welding. Confirm the actual purity and moisture requirements with the equipment supplier and gas provider.
A dark or discolored weld may indicate inadequate shielding, but it can also result from excessive heat, contamination, or other welding conditions.
Likewise, a bright weld does not automatically prove adequate penetration or the absence of internal porosity.
A useful troubleshooting guide is:
| Weld Problem | What to Check First |
|---|---|
| Discoloration | Shielding coverage, gas purity, surface cleanliness |
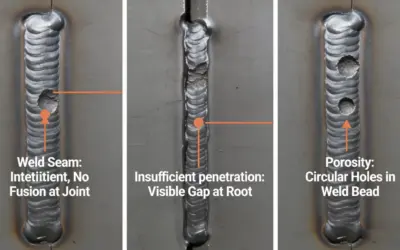
| Porosity | Contamination, leaks, gas flow, weld stability |
| Irregular Bead | Nozzle position, torch movement, flow consistency |
| Insufficient Fusion | Focus, joint fit-up, energy, travel speed |
Do not immediately replace the gas cylinder or increase laser power when a weld looks wrong.
Check the complete welding setup first.
4. How Should You Choose Between Argon and Nitrogen?
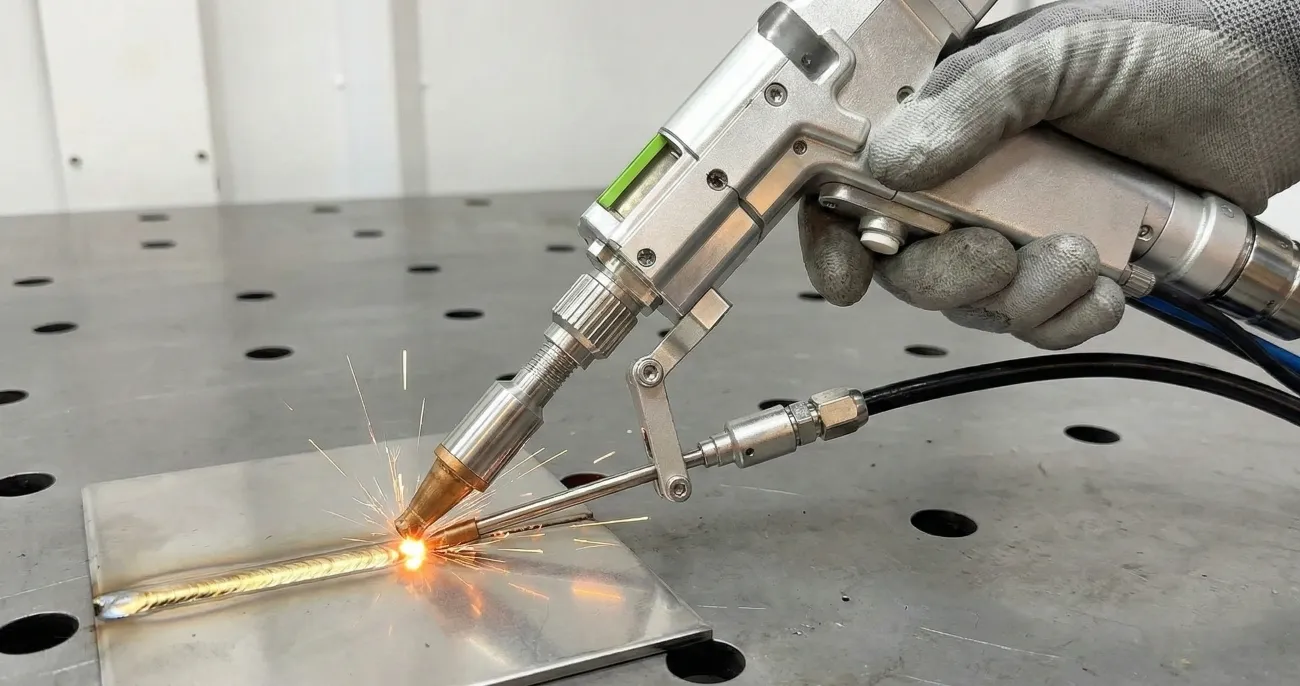
For most buyers, the decision should follow the type of work their shop performs.
Start With Your Main Material
If your business welds stainless steel, carbon steel, and aluminum throughout the week, argon is usually the most convenient starting choice.
If you manufacture one type of stainless steel component in large quantities, nitrogen may deserve a controlled comparison.
The best option depends on the production requirements—not simply which gas costs less.
Compare Weld Quality Before Cost
When comparing gases, test them on representative parts using the actual handheld fiber laser welder intended for production.
Use the same material grade, thickness, joint design, and appropriate qualified welding conditions.
Then compare the completed results.
Look at bead appearance, penetration, porosity, and any mechanical or corrosion requirements relevant to the finished product.
Do not assume that changing the shielding gas will produce the same result while every other parameter remains fixed. The process may need requalification or adjustment.
Calculate the Real Gas Cost
Nitrogen is often cheaper than argon, but the relevant number is gas cost per acceptable welded part.
Compare the gas unit price, actual flow rate, productive welding time, and any additional costs from rework or rejected components.
A cheaper gas is not more economical if it increases defects or requires additional production steps.
Likewise, paying more for argon may be unnecessary on a validated nitrogen-shielded process that consistently meets all quality requirements.
Confirm the Gas Before Production
Before standardizing your shielding gas, confirm four things:
- The gas is approved for the material and machine.
- The flow and nozzle arrangement provide adequate shielding.
- Test welds meet the required quality standard.
- Total cost per acceptable weld supports the choice.
Once the process is validated, record the gas, purity, flow rate, nozzle setup, and welding parameters.
This makes future production more consistent and reduces unnecessary adjustments between jobs.
Conclusion
Argon vs nitrogen for handheld laser welding—which shielding gas should you use?
Argon is generally the more versatile starting choice, especially for workshops welding stainless steel, carbon steel, aluminum, and other materials.
Nitrogen can be a cost-effective option for selected steel applications, particularly when the process is repeatable and has been properly tested.
For aluminum, argon remains the preferred general-purpose shielding gas.
For stainless steel, nitrogen may be suitable depending on the grade, welding requirements, and validated procedure.
However, shielding gas selection is only one part of a successful weld.
Nozzle position, gas flow, material preparation, laser parameters, and workshop airflow all affect the finished result.
Choose the gas that meets your weld-quality requirements at the lowest practical total cost—not simply the lowest cylinder price.
Our team can help review the appropriate gas options for your machine configuration and arrange application-specific sample welding before you finalize your setup. Learn more about our engineering background.

0 Comments